About Industrial Conveyor Systems
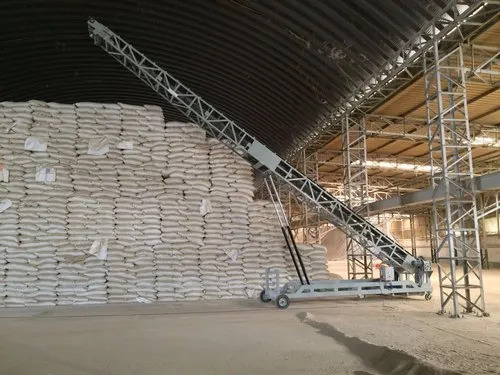
Experience soaring productivity with our Industrial Conveyor Systems, engineered for optimum efficiency in bulk material handling. Renowned for favorable reviews, these marvels are equipped with customizable lengths (10-20 meters), manual/mechanical lifts up to 12 meters, and low-noise operation (<65dB). Featuring integrated emergency stop, corrosion-resistant structure, and easy maintenance, they deliver reliable performance in harsh environments (operating from -10C to 50C). Shop now for the best price, mobile convenience, adjustable speed (up to 60 m/min), and heavy-duty capacity (2000 kg). Ideal for warehouses, mining, and agriculture in India. Manufacturer and supplier guarantee.
Superior Utility and Competitive Edge in Material Handling
Industrial Conveyor Systems are primarily used for bulk material transport in warehouses, agriculture, and mining sectors. Their mobility, modular configuration, and robust steel structure provide optimum adaptability and efficiency in various environments. Competitive advantages include low-noise operation, customizable features, integrated safety, and superior load support. The system's corrosion-resistant build and easy-maintenance design make them a reliable choice for shifting heavy loads with minimal downtime, ensuring a favorable outcome for demanding industrial operations.
Packaging, Supply, and Payment for Global Export
Our Packing & Dispatch process ensures products arrive in optimum condition, using secure and durable packaging. We offer swift dispatch to meet urgent requirements, competitive supply ability, and unbeatable pricing for bulk orders. Serving export markets as well as domestic buyers, we provide various payment terms to cater to customer convenience. Every conveyor system is prepared for transport with the lowest price offer, making us a top choice for buyers seeking value and reliability.
FAQ's of Industrial Conveyor Systems:
Q: How do Industrial Conveyor Systems benefit bulk material handling in warehouses or mining?
A: These conveyor systems deliver efficient, continuous transport of heavy loads, enhancing workflow, saving labor, and ensuring safe, steady movement of materials. Their robust structure and adjustable features allow seamless integration into different operations, maximizing productivity.
Q: What customization options are available for Industrial Conveyor Systems?
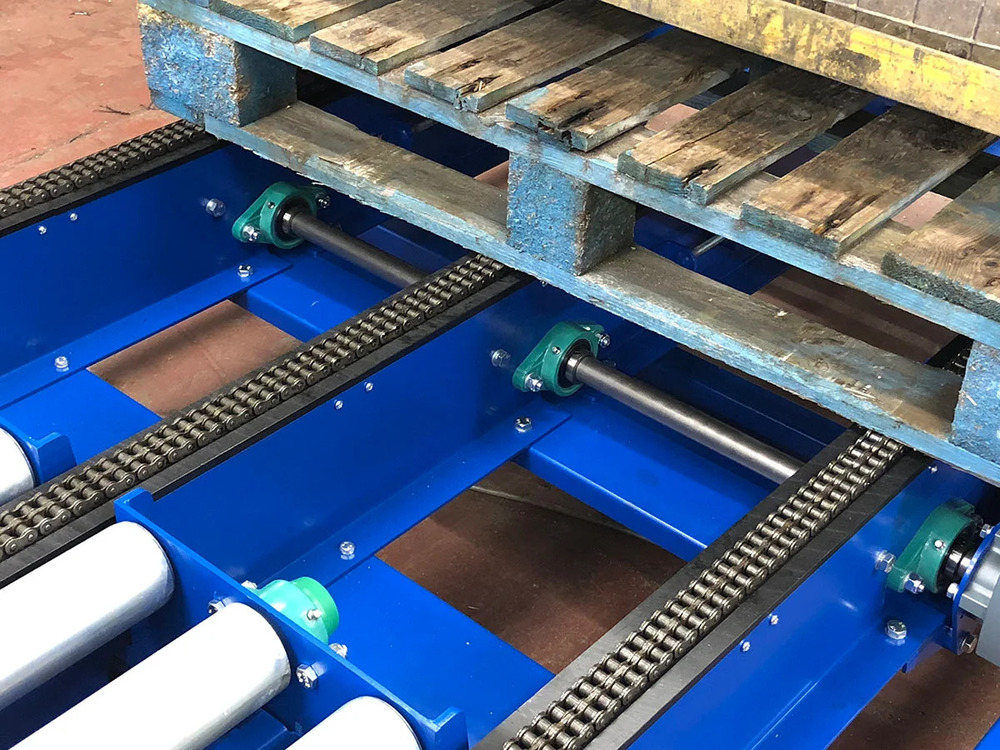
A: Conveyors can be customized for length, height adjustment, drive type, belt type, and load capacity. They can be tailored to fit specific site needs, offering options like vertical or roller conveyor attachments and adjustable inclinations.
Q: Where can these conveyor systems be used effectively?
A: Industrial Conveyor Systems are ideal for warehouses, mining, agriculture, and other bulk material handling scenarios. Their versatility allows them to operate in diverse industrial environments and demanding applications.
Q: What is the delivery process for export markets?
A: Our Packing & Dispatch protocols guarantee secure packaging and timely delivery. We support export orders with reliable logistics, competitive pricing, and flexible payment terms, ensuring the products reach international clients in pristine condition.
Q: How does the integrated safety feature work?
A: Each conveyor is equipped with an emergency stop switch, allowing quick cessation of operation during emergencies, thereby enhancing operator safety and reducing risks during handling.
Q: What kind of maintenance is required for these conveyors?
A: The design allows easy access for servicing, making routine maintenance fast and straightforward. Corrosion-resistant materials and a reinforced frame ensure longevity and reduce the need for frequent repairs.



 Send Inquiry


 Send Inquiry


