About Industrial Bucket Conveyors
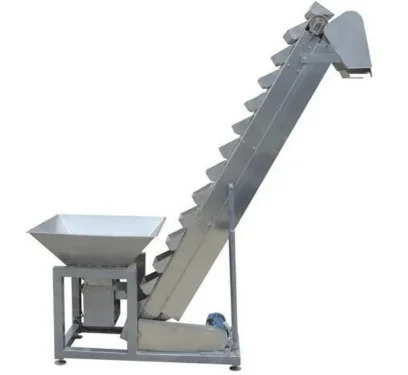
Explore the ineffable power of our Industrial Bucket Conveyors, a true masterpiece engineered for bulk material handling virtuosos. Available in high-grade plastic or metal buckets (customizable between 10-30), each unit offers a variable discharge height (up to 3 meters) and a robust feeding hopper (standard 50 liters). With an impeccable deal on automation, noise below 70 dB, and corrosion-resistant stainless steel or MS frames, enjoy effortless, safe-yet swift-operation. This sale features industry-leading options: adjustable speeds, overload protection, modular structure, and seamless maintenance. Elevate your operations-expertly, efficiently.
Tailored Solutions for Diverse Industries
Industrial Bucket Conveyors represent a reliable solution for bulk material transfer in food processing, pharmaceuticals, chemicals, and agro-industries. Their customizable heights and hopper sizes ensure smooth integration in varied operational setups. The modular structure and easy-access design make maintenance straightforward, while features like emergency stop switches and overload protection elevate safety. Resistant to corrosion and abrasion, these conveyors excel in industries demanding hygiene and rugged performance, ensuring smooth and uninterrupted handling of powders, granules, or small lumps.
Dependable Supply and Flexible Policies
Our industrial bucket conveyors offer consistent supply ability; every purchase order is handled with prioritization and care. We support clients with flexible sample policies to enable hands-on evaluation before commitment. Shipped goods are meticulously packaged, ensuring safe transit to your facility. Our primary domestic market encompasses key industrial regions across India, and each handover is professionally managed to ensure operational readiness on arrival, meeting rigorous industry standards for both delivery speed and after-sales support.
FAQ's of Industrial Bucket Conveyors:
Q: How can Industrial Bucket Conveyors be integrated into existing bulk material handling systems?
A: Industrial Bucket Conveyors can be seamlessly added to existing setups thanks to their modular structure, customizable discharge heights, and adjustable feeding hopper sizes. Floor mounting and variable drive systems enable easy compatibility with diverse processing lines.
Q: What safety features are included with these conveyors?
A: Each unit comes equipped with advanced safety provisions including overload protection and emergency stop switches. The robust frame and enclosed drive systems further minimize operational risks and enhance workplace safety.
Q: Where are these conveyors most commonly used?
A: These conveyors are widely deployed in food, pharmaceutical, chemical, and agro-industries. They are suitable for transporting bulk powders, granules, and small solids, improving efficiency wherever continuous and hygienic handling is required.
Q: What is the process for ordering and receiving an Industrial Bucket Conveyor?
A: Once a purchase order is placed, the conveyor is tailored to client specifications, subjected to quality checks, and then carefully packaged for shipment. Clients are provided regular updates until handover, ensuring timely and secure delivery of shipped goods.
Q: What are the primary benefits of choosing this conveyor system?
A: Key advantages include customizable capacity and dimensions, low maintenance needs, corrosion and abrasion resistance, smooth and low-noise operation, and operator safety enhancements-delivering superior efficiency and value for your material handling process.



 Send Inquiry


 Send Inquiry


